Answer first: what should the buyer decide?
The central issue in air compressor selection for farm equipment maintenance is service air for distributed agricultural equipment. Do not begin with horsepower, tank size or a familiar brand name. Begin with the work that the compressed air must perform, then convert that requirement into pressure at the point of use, usable airflow, duration and environmental constraints. That sequence prevents a common procurement error: buying a compressor that looks large enough but does not deliver the required air under the real operating condition.
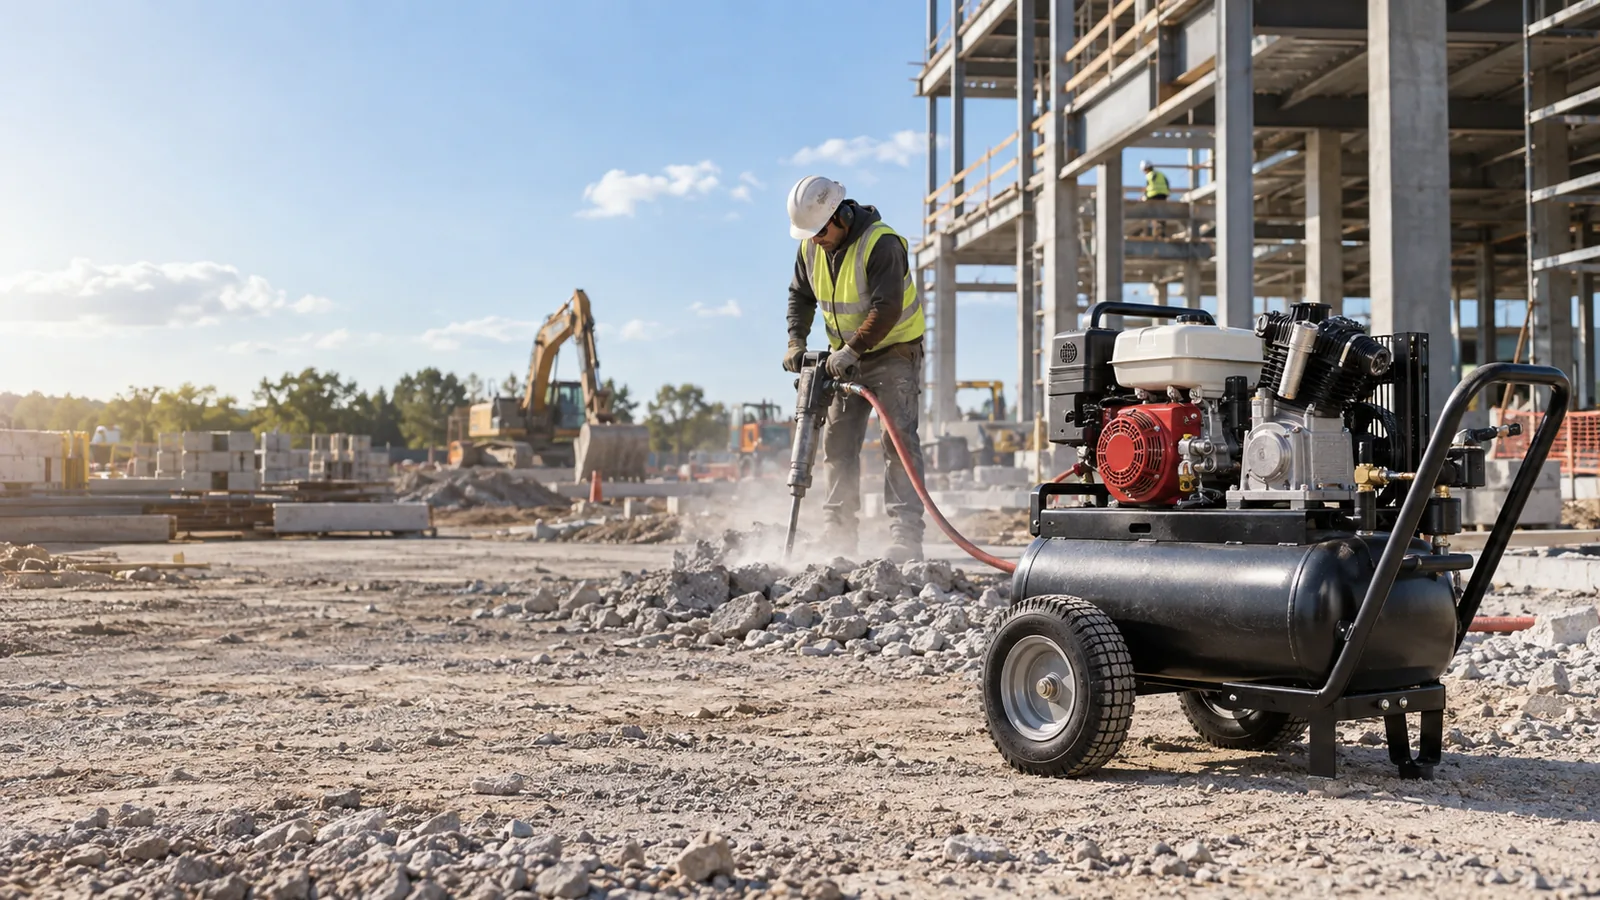
Typical examples include tractor tires, cleaning and machinery maintenance. The practical checks are mobility, dust, hose distance, pressure, flow and rugged placement. These variables interact. A pressure loss caused by a small hose can make an adequate compressor appear undersized; a large receiver can hide a peak for a few minutes but cannot support an undersized compressor indefinitely; a high ambient temperature can reduce cooling margin even when the pressure and flow numbers look correct.
Translate the application into pressure and flow
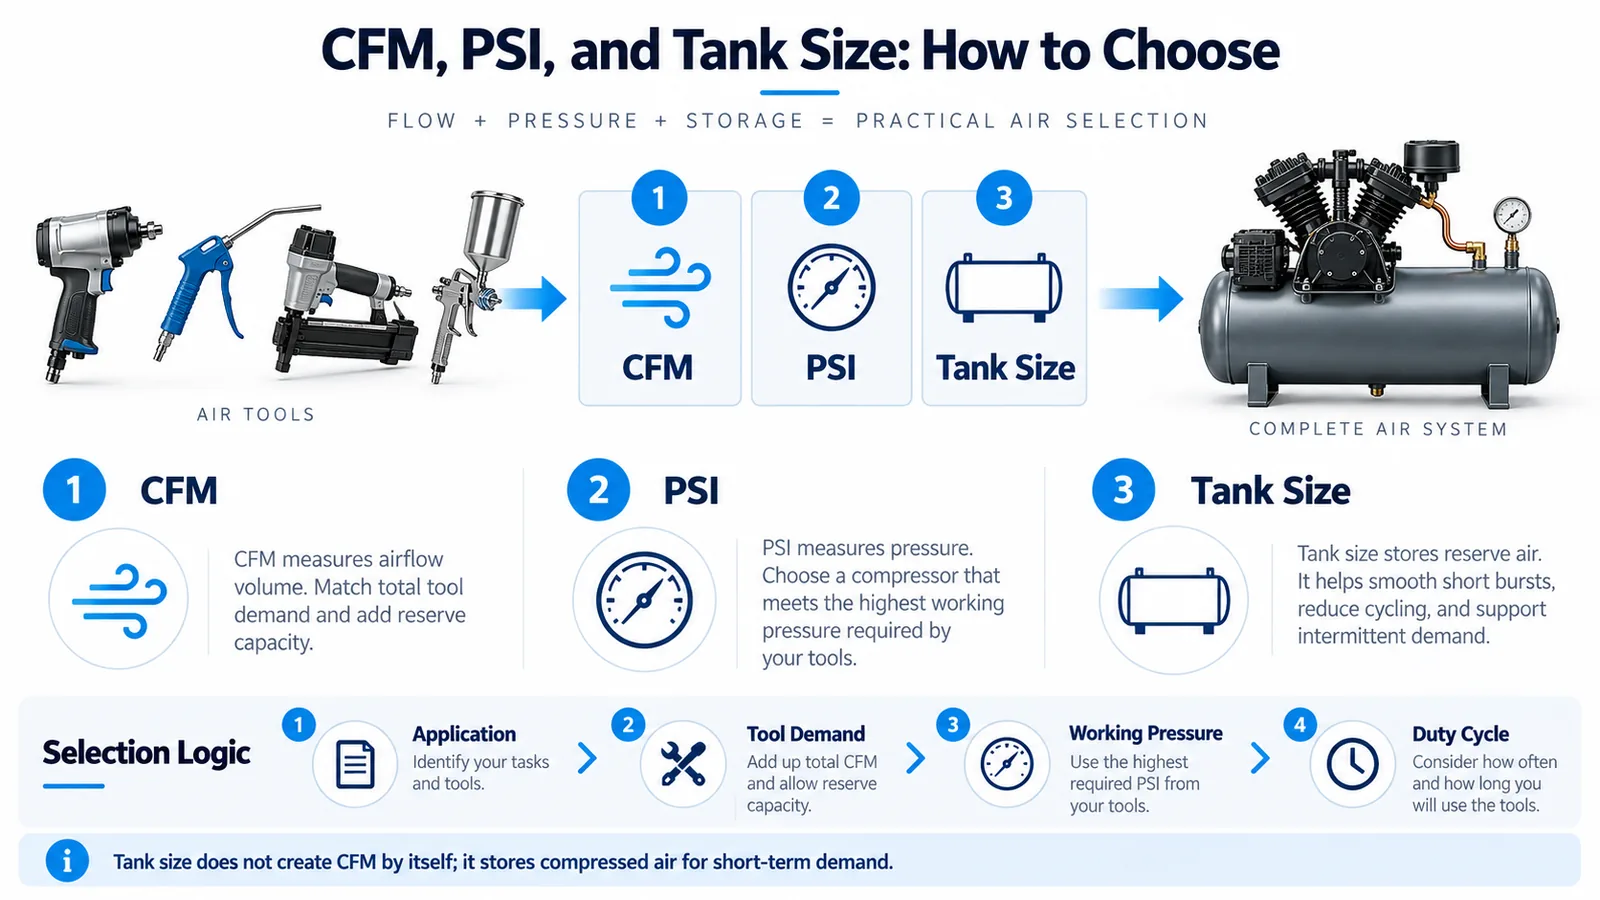
Write down the required working pressure for each air consumer and measure or obtain its flow demand. If several devices can run at the same time, add the simultaneous demand rather than the total installed demand. For intermittent tools, use a realistic duty factor but keep short peaks visible. The compressor must recover from those peaks without spending the entire shift at an unstable pressure.
Pressure should be specified at the user, not only at the compressor outlet. Distribution pipe, filters, dryers, valves, quick couplers and flexible hose all consume pressure. The longer the run and the greater the flow, the more important diameter and layout become. A good specification distinguishes compressor discharge pressure from minimum acceptable point-of-use pressure and states the expected pressure drop budget.
Understand the role of receiver storage
A receiver stores compressed air and dampens short differences between compressor output and demand. It can reduce rapid cycling and help a system tolerate brief peaks, but it does not create air. During a sustained load, the pressure continues to fall if consumption exceeds compressor delivery. That is why tank capacity and compressor free-air delivery must be considered together.
Receiver selection should also account for drainage and inspection access. Compressing air raises its temperature; as the air cools, moisture can condense. Humid climates and long run times can produce significant water. Automatic drains can reduce manual work, but they still need inspection. Downstream air quality requirements may justify a dryer, coalescing filtration or additional treatment beyond the receiver.
Match compressor architecture to duty cycle
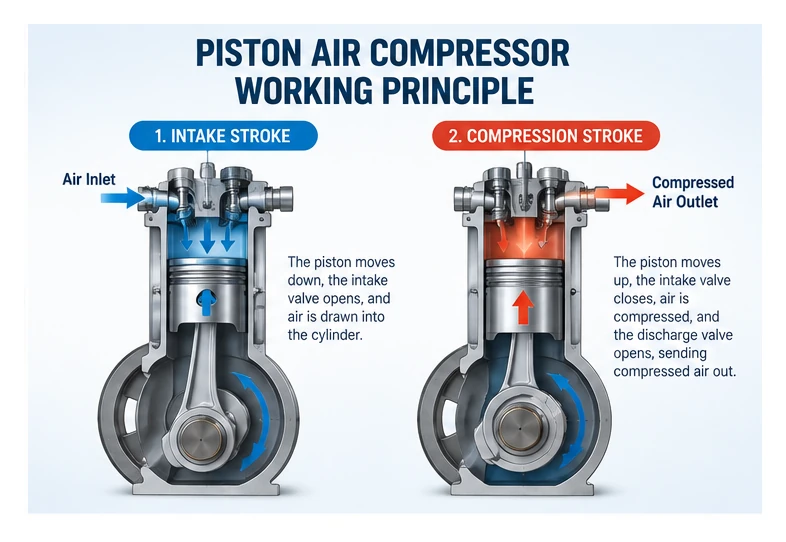
Piston or modular receiver compressors are often effective when demand is intermittent and stored air can carry short peaks. Screw compressors are strong candidates for long, stable operating periods because the compression process is continuous. Oil-free architectures are selected when contamination risk from the compression chamber matters, while micro-oil systems may be appropriate when process requirements allow lubricant management and downstream treatment.
The choice should reflect operating hours, starts per hour, load variation, maintenance capability and installation environment. A workshop that runs an impact wrench for seconds at a time does not resemble a production line consuming air throughout a shift. Likewise, a 20–40 bar process cannot be treated as a standard 8 bar workshop system simply by increasing a pressure setting; the compressor architecture and every downstream pressure-rated component must be appropriate.
Plan the installation as part of performance
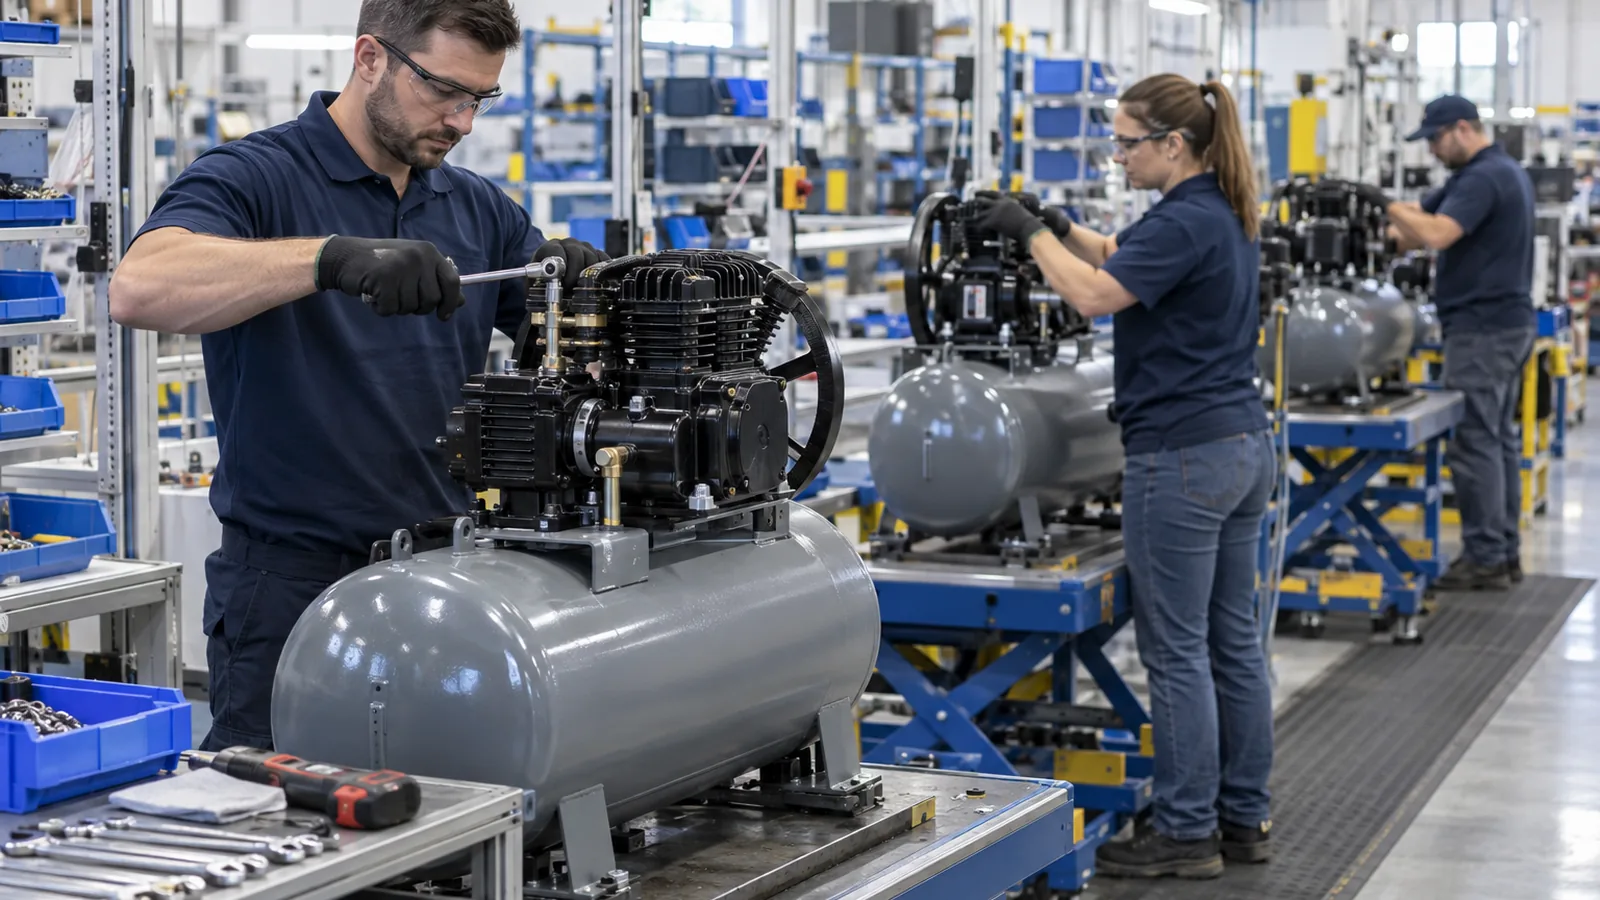
Compression creates heat. Put the machine where cool intake air is available and where hot discharge air can leave without recirculating. Maintain service clearances around filters, panels, drains and cooling surfaces. A compressor packed tightly into a small room can run hotter, become harder to maintain and deliver less reliable service even when its nameplate selection was correct.
Electrical planning includes voltage, frequency, phase, protection, conductor sizing and grounding. Export projects should confirm the destination supply before production. On the air side, size pipe for the expected flow, minimize unnecessary restrictions, slope and drain distribution where appropriate, and isolate equipment so service work does not require shutting down unrelated users. For high-pressure systems, confirm the pressure rating of every downstream component.
Use a commissioning baseline for future troubleshooting
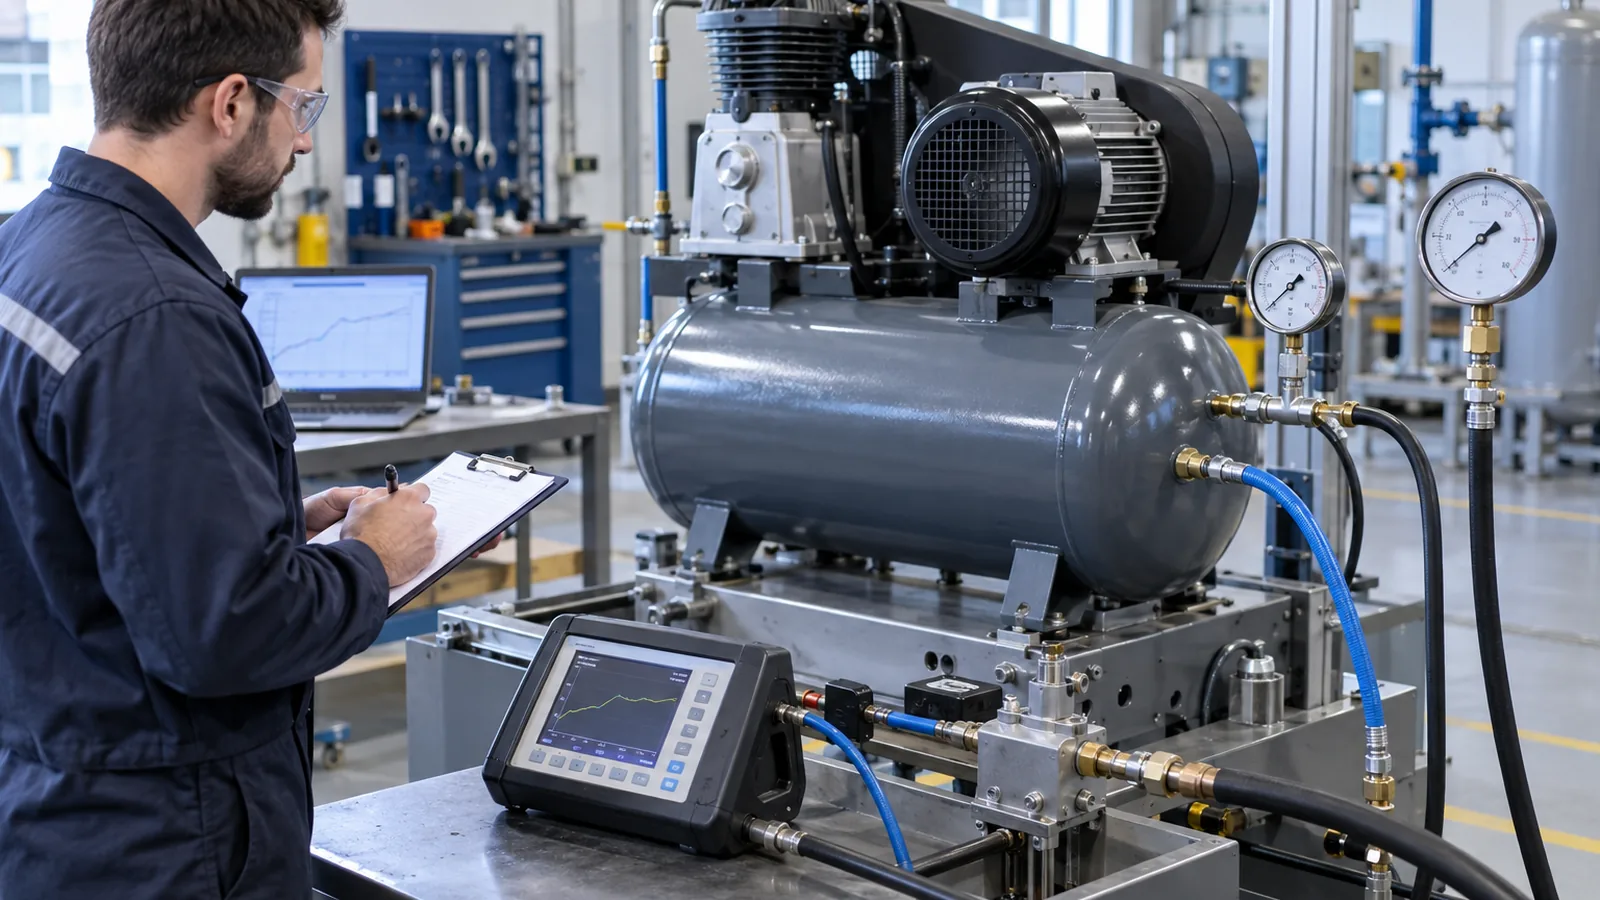
Before the equipment enters normal service, record no-load and loaded pressure, running current, recovery time, temperature, drain behavior and any normal sound or vibration. Check for leaks at connections and confirm that controls unload, stop or regulate as intended. A baseline makes later diagnostics much faster because maintenance personnel can compare a new symptom with known healthy behavior.
If pressure later falls, start with system observations. Check whether demand increased, whether a valve was left open, whether filters are restricted and whether new leaks developed. If temperature rises, inspect cooling surfaces, ventilation and intake conditions before assuming an internal compressor fault. A disciplined sequence avoids replacing expensive components when the cause is external.
Maintenance priorities that protect usable air
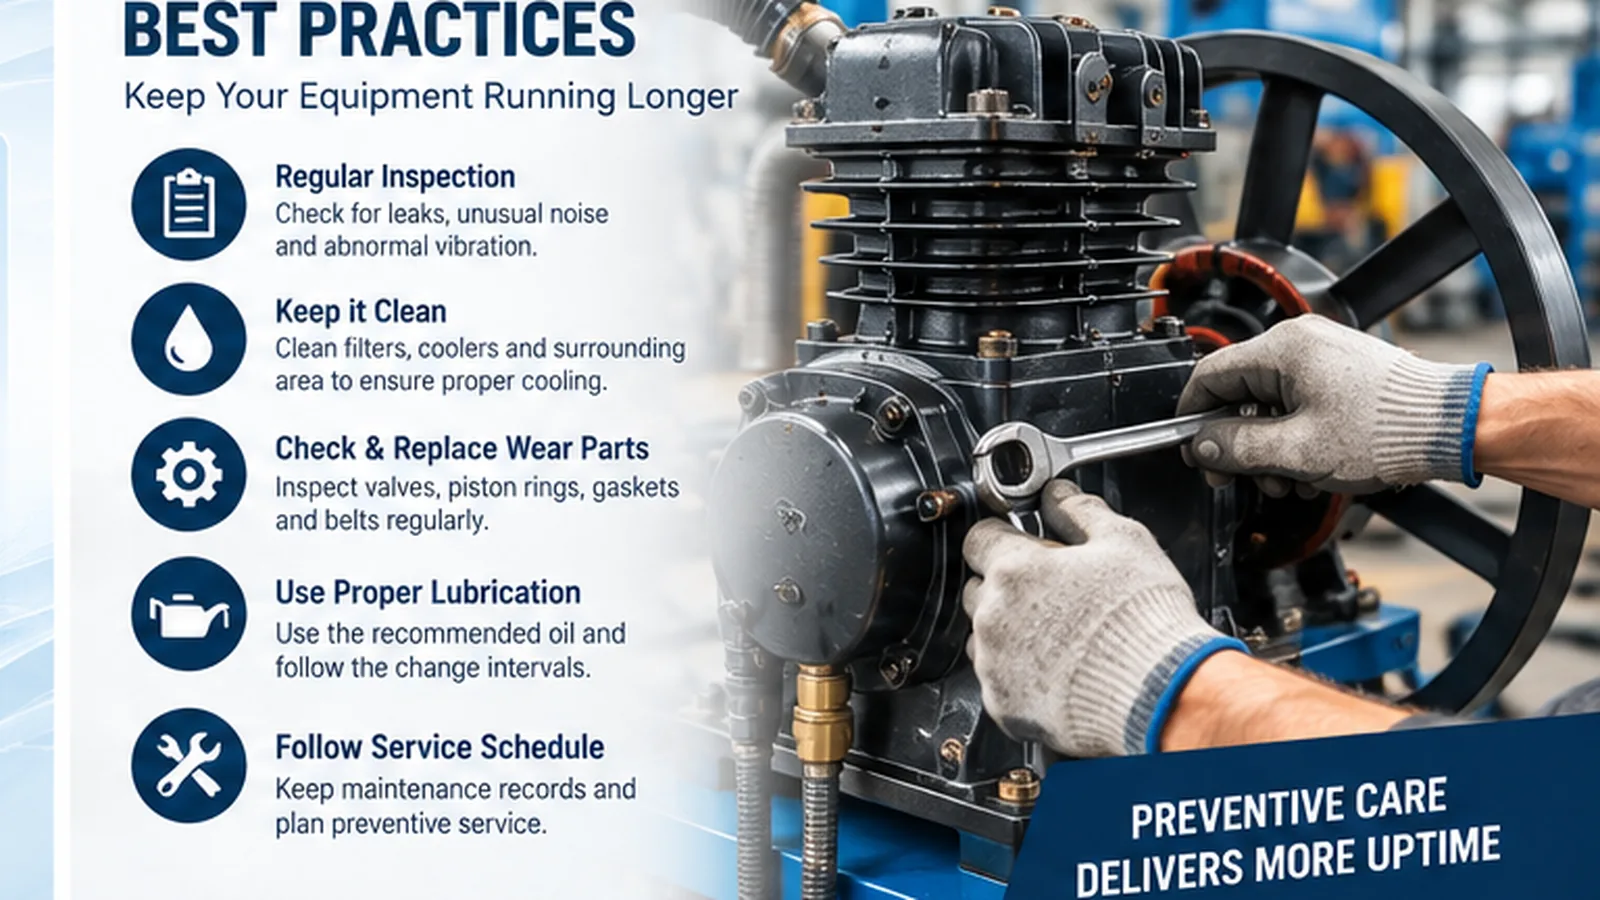
Maintenance should preserve airflow, cooling, sealing and control. Keep intake filters clean, drains functional and fittings tight. Follow the specified lubricant or water-circuit requirements for the compressor technology in use. Check belts, couplings or drive components where fitted. Clean coolers before dirt becomes a thermal restriction. Record service dates, running hours and any change in pressure or temperature.
Leak management belongs in the maintenance program because leaks can consume capacity continuously. Repairing leaks can restore pressure and defer unnecessary compressor expansion. In dusty or humid environments, inspection frequency may need to increase. The objective is not to perform more maintenance; it is to detect degradation early enough that the system continues to supply the required air efficiently and predictably.
Procurement checklist for farm air compressor
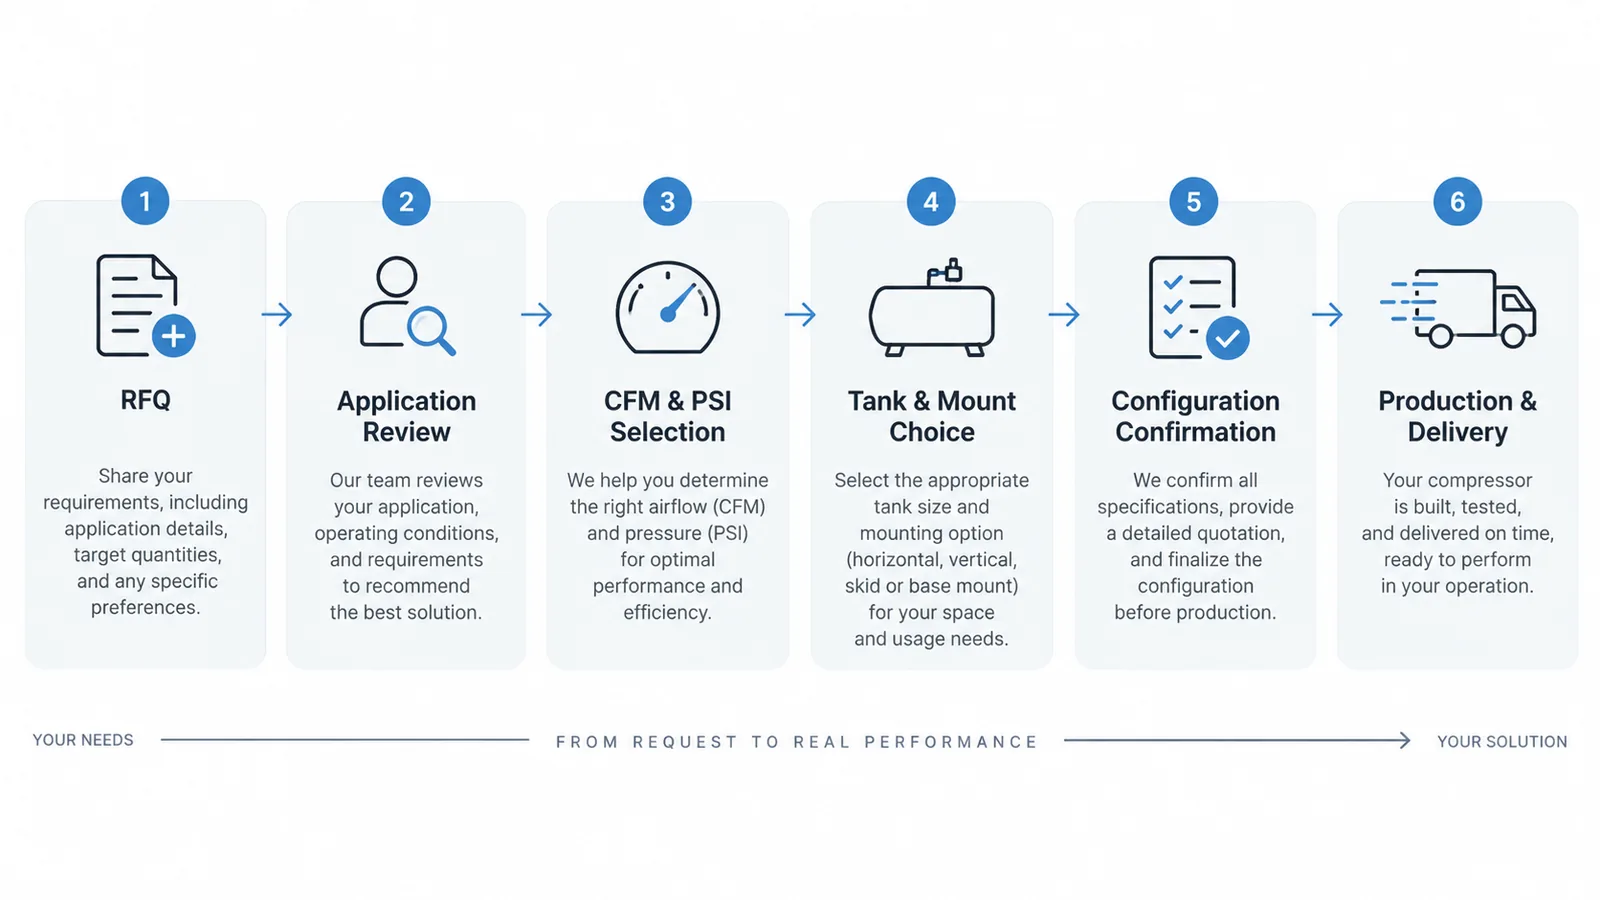
Send pressure at the point of use, required airflow, peak duration, operating hours per day, voltage/frequency/phase, ambient conditions, air-quality requirements, quantity, destination and installation constraints. If an existing compressor is being replaced, include the current model, pressure setting, measured load behavior and the reason for replacement. If the system is new, identify the pneumatic consumers instead of guessing a compressor size.
For process equipment, add connection size, allowable pressure variation and any required drawings or documentation. For outdoor or mobile service, include weather, dust, portability and access constraints. For clean processes, define the contamination limit rather than relying on a vague description such as “clean air.” The more clearly the boundary conditions are stated, the more useful the quotation and technical review will be.
Related planning: review compressor families, use the selection guide, and compare application requirements.
Frequently asked questions
Is maximum pressure enough to choose a compressor?
No. The system must deliver sufficient airflow at the working pressure. Maximum pressure alone does not describe usable capacity.
How much spare capacity should I add?
Add a documented allowance for realistic leakage, uncertainty and planned growth. Avoid arbitrary oversizing that hides weak demand data.
Does a bigger receiver always improve performance?
It improves short-term storage and can reduce cycling, but sustained demand still depends on compressor delivery.
What data should be measured on an existing system?
Measure loaded pressure, point-of-use pressure, run/load pattern, recovery behavior and, when available, actual flow. Also identify leaks, restrictions and treatment pressure drop.
Field measurements that make the decision defensible
For Air Compressor Selection for Farm Equipment Maintenance, the useful starting point is to translate the actual tools or process into simultaneous airflow, minimum pressure and a realistic duty pattern instead of choosing from tank size alone. Build the record around tool air consumption, number of simultaneous users, minimum point-of-use pressure, hose and pipe length, peak duration, recovery time, receiver size, ambient dust or humidity and daily operating hours. A single gauge reading taken when demand is low is not enough. Capture the condition during the heaviest realistic operating period, and note which tools, valves, filters, dryers or production steps are active at the same time. That makes the data repeatable and helps another engineer understand why the selected configuration was considered adequate.
Measurements should be paired with context. Note whether the compressor is fully warmed, whether ambient temperature is unusually high, whether drains are operating and whether the distribution system has recently been changed. Where pressure drop is suspected, compare a reading close to the compressor with one at the critical user while the same load is running. For application sizing, this simple comparison often reveals whether the next action belongs at the compressor, in storage and controls, or in the distribution system.
Decision matrix: what to compare before changing equipment
| Decision point | What to verify | Why it matters |
|---|---|---|
| Operating point | tool air consumption, number of simultaneous users, minimum point-of-use pressure, hose and pipe length, peak duration, recovery time, receiver size, ambient dust or humidity and daily operating hours | The machine must be judged at the pressure and duty that the application actually uses, not from a headline motor or tank figure. |
| System losses | Pressure before and after treatment, piping and flexible hose during peak demand. | A restriction can create the same symptom as insufficient compressor capacity, but requires a different corrective action. |
| Installation margin | keep hose runs practical, avoid restrictive couplers, provide drainage and clean intake air, protect the machine from dust and recirculated heat, and position the receiver and controls where routine checks are possible | Cooling, access, drainage and distribution conditions determine whether documented performance can be maintained in service. |
| Acceptance method | run the heaviest realistic tool combination, record compressor and point-of-use pressure, verify recovery after a peak, inspect for leaks and confirm that the electrical or engine supply remains stable | Defining the check in advance prevents disagreement between procurement, maintenance and the supplier after startup. |
The comparison should be based on the same units and test basis throughout the project. If airflow is quoted at different pressures or under different reference conditions, normalize the comparison before drawing conclusions. A clear decision table is especially useful when several close models are being considered, because it exposes the reason for choosing one configuration rather than simply recording the final model number.
Installation checks that protect the expected performance
Keep hose runs practical, avoid restrictive couplers, provide drainage and clean intake air, protect the machine from dust and recirculated heat, and position the receiver and controls where routine checks are possible. Confirm these items before commissioning because installation deficiencies can consume the margin that was available during sizing. A long run of undersized pipe, a dirty inlet location or hot discharge air returning to the intake can reduce usable performance without any change to the compressor itself. The installation drawing should show isolation, drainage, treatment equipment and the route to the critical users so pressure-loss and service-access questions can be reviewed before the machine is fixed in place.
After installation, inspect the system under load rather than relying only on an idle test. Verify that piping is supported, flexible connections are not strained, condensate can be removed, panels and filters remain accessible, and the cooling path is not blocked by walls or stored material. For electrical machines, confirm the actual supply and protection; for any higher-pressure circuit, verify the pressure rating of every downstream component. These checks turn the article guidance into a commissioning action rather than a generic recommendation.
How to read abnormal behavior without jumping to the wrong cause
During application sizing, slow tools, falling pressure during long use, frequent cycling or long recovery can come from insufficient delivery, leakage, restricted hose, poor storage strategy or a combination of those factors. The sequence of the symptom matters. A gradual loss that develops over weeks should be investigated differently from a change that appears immediately after maintenance, a new production load or a piping modification. Record the first observable change, the load at which it occurs and whether pressure, temperature, noise, current or recovery time changed together. Those relationships are often more diagnostic than the absolute value of any one measurement.
Use low-cost external checks before opening major components. Confirm demand, valve position, filter condition, leakage, drains, cooling and supply conditions. If the symptom persists, compare the current readings with the commissioning baseline. Escalation is justified when the system-side checks are normal but performance remains outside the documented operating range. This approach reduces unnecessary parts replacement and preserves a clear troubleshooting history for the next service event.
Commissioning record and acceptance criteria
A useful acceptance record for Air Compressor Selection for Farm Equipment Maintenance should state the operating condition and the result, not only mark a box as “pass.” At minimum, run the heaviest realistic tool combination, record compressor and point-of-use pressure, verify recovery after a peak, inspect for leaks and confirm that the electrical or engine supply remains stable. Add the ambient condition and the active air consumers so the data can be reproduced later. If the project includes air treatment, also note the pressure drop across the treatment train and the drain condition. If a performance point is contractually important, agree on the measurement method before testing.
Keep this baseline with the maintenance record. It gives technicians a reference for deciding whether a future change is normal variation or evidence of restriction, leakage, fouling, control drift or changed demand. When a system is expanded, repeat the same measurements with the new load rather than assuming the original spare margin is still available. A consistent acceptance method is one of the simplest ways to make compressor selection, commissioning and maintenance part of one engineering process.
RFQ data that reduces back-and-forth
For a quotation or configuration review, provide tool list, simultaneous-use assumption, required pressure, hose distance, operating hours, peak duration, available power, mobility needs, environment, quantity and destination. Where a value is uncertain, say that it is unknown and identify the tool, process or existing machine that creates the requirement. That is more useful than inserting an arbitrary number, because the supplier can see which assumption still needs verification. If an existing installation is being replaced, include its model, the pressure actually used, the observed load behavior and the reason for replacement.
Use the RFQ to define the boundary of supply as well as the compressor. State whether the receiver, dryer, filters, drains, starter or controls are part of the requested package, and identify any dimensional or connection constraints. For export projects, destination and electrical supply should be confirmed before production. For critical applications, include the expected acceptance record so both sides understand how the selected configuration will be checked after installation.